

SEPARATORS
BUY REDA SEPARATORS
REDA RE-P series self-cleaning separators are used in the dairy industry to improve milk quality. By removing solid impurities like dirt, straw, hair, sand, blood residues, udder cells, and various somatic cells, bacteria, and spores, these separators enhance milk clarification and ensure higher-quality dairy products. Designed for processing raw milk from various sources, including cow, sheep, and goat, these clarifiers can operate in both warm and cold conditions.
iFlow are exclusive distributors for REDA clarifiers & separators – contact us to buy Reda separators.
CLARIFIERS
CLARIFIERS FOR MILK RE-P
|
|
|
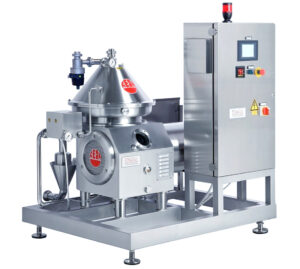 |
Product OverviewREDA RE-P series self-cleaning separators are used in the dairy industry to improve milk quality. By removing solid impurities like dirt, straw, hair, sand, blood residues, udder cells, and various somatic cells, bacteria, and spores, these separators enhance milk clarification and ensure higher-quality dairy products. Designed for processing raw milk from various sources, including cow, sheep, and goat, these clarifiers can operate in both warm and cold conditions. The RE-P series features a soft flow inlet system that gently accelerates the milk to the optimal clarification speed, preserving the fat quality, which is especially important for sheep and goat milk. The separator’s wide working surface and rapid sludge expulsion ensure high clarification efficiency and a significant reduction in bacterial load. |
Applications
|
|
Downloads |
|
CLARIFIERS FOR JUICE RE-V/EO
|
|
|
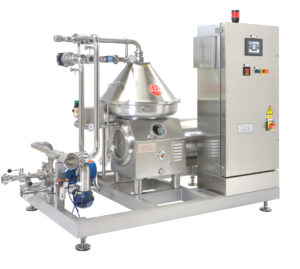 |
Product OverviewClarifiers for Juices RE-V/EO REDA separators are synonymous with quality and performance, and we ensure that every RE-P centrifuge model upholds these standards. Our clarifiers are specifically engineered for the clarification of non-alcoholic beverages, efficiently separating and ejecting heavier solids. To cater to diverse producer requirements, we provide a broad range of sizes and designs, including economical, compact top-fed technologies and fully hermetic feeding options. The RE-P series features a standard design with an expansive operational surface and automatic solids ejection capabilities, delivering exceptional clarification efficiency. This design enables continuous clarification in a single pass, even with high flow rates and significant solids content, eliminating the need for recirculation. The hermetic construction ensures gentle product handling, prevents oxidation, maximises yield and quality, and optimises energy consumption through the use of gear drives controlled by inverters across all models. In many applications, our clarifiers are an essential pre-clarification tool before membrane filtration processes (e.g., apple juice fining), ensuring high yields, large capacities, and superior final product quality. |
Applications
|
|
Downloads |
|
CLARIFIERS FOR MUST, WINE RE-V/AP/S
|
|
|
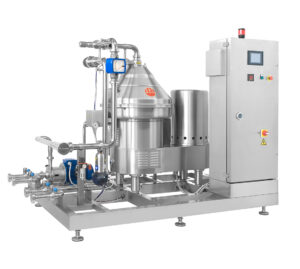 |
Product OverviewThe RE-V series separators are specifically designed for the wine industry, offering high versatility and an environmentally friendly approach to wine processing. These separators are ideal for clarifying white grape must, young wines, and matured wines, ensuring efficient cleaning and improved wine quality. Key benefits of the RE-V series separators include:
|
Applications
|
|
Certifications |
|
Downloads |
|
CLARIFIERS FOR BEER RE-BR
|
|
|
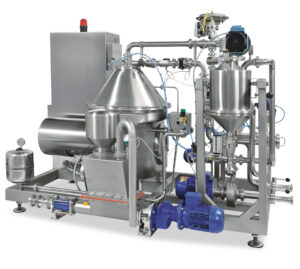 |
Product OverviewThe REDA Clarifiers of the RE-BR series are a highly efficient solution for beer clarification. Their automated control system ensures a continuous process, expelling solids without interruptions for cleaning, making them particularly user-friendly for large-scale operations. The standout feature is the ZeroOx™ hermetic system, exclusive to REDA, which prevents oxygen absorption during processing. This innovation is designed to protect the beer’s quality, avoiding protein damage and foam reduction, ensuring a perfect draught every time. The large operational surface and automatic ejection of solids make these clarifiers efficient and effective, offering excellent separation of yeast, solid hop residues, and tank bottoms. |
Applications
|
|
Downloads |
|
CLARIFIERS FOR SPECIAL PRODUCTS RE-P/SA
|
|
|
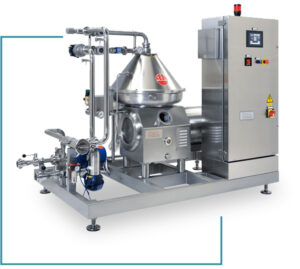 |
Product OverviewThe RE-P/SA clarifiers are designed for highly specialized applications, prioritizing precision and delicacy in the separation and concentration of sensitive products. These centrifuges deliver reliable, repeatable results with exceptional clarity and high concentration, which makes them particularly well-suited for industries where product integrity is crucial. Their fast processing and accuracy seem ideal for such applications where precision and care are key. |
Applications
|
|
Downloads |
|
SEPARATORS
MILK SEPARATORS RE-T/TE
|
|
|
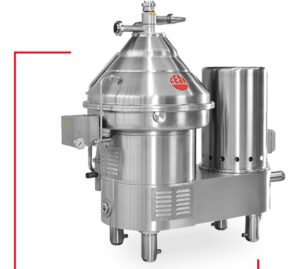 |
Product OverviewREDA RE-T/TE series self-cleaning separators are designed for fat separation in raw milk before processing. These centrifuges can perform various functions like total skimming, partial skimming (fat standardisation), or simply milk cleaning. Key features and benefits of the RE-T/TE series include:
|
Applications
|
|
Downloads |
|
WHEY SEPARATORS RE-W
|
|
|
 |
Product OverviewREDA RE-W series separators are designed for full skimming of whey to recover valuable residual fat. These separators are specifically designed for the dairy industry and offer high efficiency in separating fat globules from whey. Key features and benefits of the RE-W series include:
|
Applications
|
|
Downloads |
|
BACTERIA SEPARATORS
|
|
|
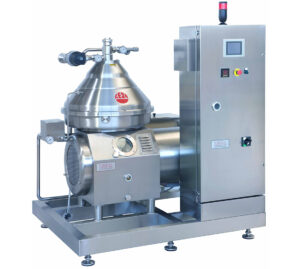 |
Product OverviewREDA bacteria-removing separators are designed to improve milk quality by continuously removing bacteria and spores. This is achieved by separating impurities from the milk, addressing issues like acid fermentation, cheese blowing, and reduced shelf life caused by bacterial contamination. As many spores are resistant to heat treatment, bacteria removal is crucial for enhancing the quality and shelf life of fresh milk. |
Applications
|
|
Downloads |
|
AUTOMATIC STANDARDISERS
RTM SERIES
|
|
|
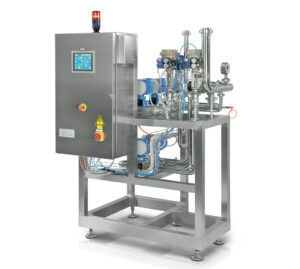 |
Product OverviewREDA RTM series automatic standardizers offer an efficient solution for in-line milk and cream standardisation. By combining standardisation with the skimming process, these units eliminate the need for manual mixing and reduce time and costs associated with traditional methods. Key benefits of the RTM series standardizers include:
|
Applications
|
|
Downloads |
|
Explore other brands

iFlow are an exclusive distributor for REDA clarifiers & separators
Reda is a leading manufacturer of Separators, Clarifiers, Bactofuges and Standardisers. With many years of experience in this field, Reda specialises in the separation of Fats and clarification of Curd Whey, Beer, Wine, Juice and Natural Fruits
Explore other brands
iFlow is an exclusive distributor for Bardiani Valvole
Bardiani Valvole is a leading manufacturer of sanitary valves for the food, beverage, dairy, pharmaceutical, and cosmetic industries. With decades of experience in hygienic process engineering, Bardiani specialises in the design and production of butterfly valves, single and double seat valves, mixproof valves, and control valves, offering reliable solutions for the safe and efficient handling of liquids in demanding sanitary environments.
Explore other brands
iFlow are authorised distributors for CSF Inox Spa
CSF Inox are a global leader in the production of hygienic pumps, primarily designed for the Food, Beverage, Chemical and Pharmaceutical process industries. The pumps are manufactured to the highest quality standards, offering a wide selection to meet the demands of even the most challenging fluid handling applications.
Explore other brands

iFlow are exclusive distributors for OMAC Pumps
OMAC is the only Italian company specialising in the production of volumetric Lobe Pumps made from AISI 316L stainless steel and special alloys such as Hastelloy, Monel and Titanium. The current range is the result of years of experience acquired through working with leading companies in the Food, Beverage, Chemical, Cosmetic and Pharmaceutical sectors.
Explore other brands
iFlow are exclusive distributors for MBS SRL
MBS SRL are experts in the heat treatment of Food, Drinks, Chemicals and Pharmaceuticals. Using quality raw materials and lean production methods, MBS manufacture a comprehensive range of Tubular Heat Exchangers and Scrape-surface Heat Exchangers for all types of fluid handling applications.
Explore other brands

iFlow are exclusive distributors for Debem
Debem hygienic Air Diaphragm Pumps are specially designed for handling an array of products in the Dairy, Food, Beverage, Cosmetics, Chemical and Pharmaceutical industries. Manufactured in high quality 316L, Debem Pumps offer complete flexibility and are ideal for ATEX pumping applications or handling products containing solids.
Explore other brands

iFlow are exclusive distributors for INCON tanks & vessels
Incon design and manufacture mobile stainless tanks ranging from 100 ltr to 2,500 ltr for use with storing and transporting a wide range of liquids. Many different designs are available to suit all types of applications including Tanks for use with Fork Trucks, Pallet trucks and Stand alone Tanks on wheels.
Explore other brands
iFlow are exclusive distributors for FBF Italia Homogenisers
FBF Italia design and manufacture Homogenisers and High-pressure Pumps to suit a wide range of applications in the food, Beverage, Chemical, Cosmetic and Pharmaceutical industries. Through many years of continuous research, FBF Italia continue to deliver high quality machines tailored to specific individual customer needs.
Copyright 2025 - Website design by Sian Evans Inc
Contact
+44 (0)208 180 2204
info@iflow.co.uk
Offices
UNIT A1B LORDS WOOD ROAD
HARWORTH, DONCASTER DN11 8BZ