

HOMOGENISERS
BUY FBF HOMOGENISERS
iFlow – Leading suppliers in Hygienic and Sterile Processing Equipment for the Food & Beverage industries. We are UK distributors for the very best family owned Italian Equipment Manufacturer’s. Including: CSF Inox, Bardiani, OMAC, MBS, Reda, FBF, Laveggi, Incon, Burocco and Bolondi. We pride ourselves on our dedication to provide quality equipment at competitive prices.
HOMOGENISERS
INDUSTRIAL HOMOGENISERS
|
|
|
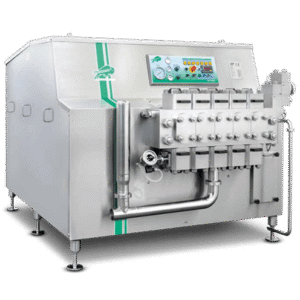 |
Product OverviewIndustrial homogenisers play a crucial role in the mixing and micronisation of product components, delivering uniform, stable textures across a wide range of applications. This technology is essential in industries where product consistency, quality, and shelf stability are non-negotiable. Homogenisation is widely applied across the food and beverage, chemical, pharmaceutical, and cosmetic sectors, enabling manufacturers to achieve optimal results in both texture and formulation integrity. All homogenisers in our range are designed and manufactured in full compliance with European Community (EC) regulations, ensuring the highest standards of safety, hygiene, and reliability. These systems are built to meet the needs of both small-scale production and high-capacity industrial processing. Key Features
Whether you are producing emulsions, suspensions, or pastes, our industrial homogenisers offer the flexibility and control required for consistent, high-quality results. |
Applications
|
|
Downloads
|
|
LABORATORY HOMOGENISERS
|
|
|
 |
Product OverviewFBF Italia’s laboratory homogenisers are engineered to deliver highly reliable test data, enabling seamless translation from R&D to full-scale production. Unlike conventional single-piston designs, these homogenisers feature a dual-pumping piston configuration, ensuring consistent pressure and greater process stability during sample testing. This innovation provides more accurate, reproducible results, making it easier to define and replicate optimal homogenisation conditions in industrial manufacturing environments. The range includes two models tailored to laboratory-scale applications: Homolab 2.20 Homolab 2.50 Both models are designed for ease of use, reliability, and long-term performance in laboratory settings where data integrity and repeatability are critical. |
Applications
|
|
Downloads |
|
ICE CREAM HOMOGENISERS
|
|
|
 |
Product OverviewThe Microlab 400 by FBF Italia is redefining quality and performance in both artisan and industrial ice cream manufacturing. Traditionally, the adoption of industrial homogenisation in small-scale or artisan settings has been limited due to issues such as cost, equipment size, operational complexity, and lack of performance data specific to ice cream production. The Microlab 400 overcomes these barriers with a compact, high-performing solution tailored to the unique needs of ice cream manufacturers. At the heart of the process is a high-pressure homogenising valve. The product is drawn in by pumping pistons and forced through the valve at high speed and pressure. During this phase, the mixture undergoes micronisation through a combination of sudden acceleration (up to 9,300 cm/sec), cavitation, and friction between particles. This results in fat globules being reduced to less than 3.5 μm, significantly increasing their surface area and improving interaction with emulsifiers. This level of homogenisation enhances the stability of the water-oil phase, delivering a finished product with improved texture and mouthfeel. The result is ice cream that is creamier, more flavourful, and more consistent in quality. Key Benefits of the Microlab 400
The Microlab 400 brings laboratory-level homogenisation performance to ice cream manufacturers seeking to elevate their product quality while maintaining production efficiency. |
Applications
|
|
Downloads |
|
VOLUMETRIC PUMPS
|
|
|
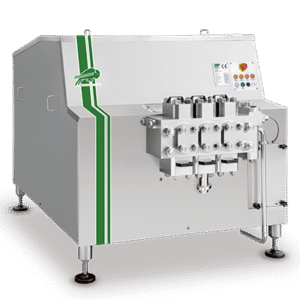 |
Product OverviewFBF Italia’s positive displacement pumps are engineered with the same high standards and design principles as their industry-leading homogenisers. The key distinction lies in the absence of the homogenisation head, making them ideal for applications where high-pressure mixing is not required. These pumps are widely used across the food and beverage, chemical, pharmaceutical, and cosmetic industries, where consistent flow, product integrity, and durability are essential. Built for performance, reliability, and hygiene, FBF Italia positive displacement pumps offer a trusted solution for demanding processing environments. |
Applications
|
|
Downloads |
|
Explore other brands

iFlow are an exclusive distributor for REDA clarifiers & separators
Reda is a leading manufacturer of Separators, Clarifiers, Bactofuges and Standardisers. With many years of experience in this field, Reda specialises in the separation of Fats and clarification of Curd Whey, Beer, Wine, Juice and Natural Fruits
Explore other brands
iFlow is an exclusive distributor for Bardiani Valvole
Bardiani Valvole is a leading manufacturer of sanitary valves for the food, beverage, dairy, pharmaceutical, and cosmetic industries. With decades of experience in hygienic process engineering, Bardiani specialises in the design and production of butterfly valves, single and double seat valves, mixproof valves, and control valves, offering reliable solutions for the safe and efficient handling of liquids in demanding sanitary environments.
Explore other brands
iFlow are authorised distributors for CSF Inox Spa
CSF Inox are a global leader in the production of hygienic pumps, primarily designed for the Food, Beverage, Chemical and Pharmaceutical process industries. The pumps are manufactured to the highest quality standards, offering a wide selection to meet the demands of even the most challenging fluid handling applications.
Explore other brands

iFlow are exclusive distributors for OMAC Pumps
OMAC is the only Italian company specialising in the production of volumetric Lobe Pumps made from AISI 316L stainless steel and special alloys such as Hastelloy, Monel and Titanium. The current range is the result of years of experience acquired through working with leading companies in the Food, Beverage, Chemical, Cosmetic and Pharmaceutical sectors.
Explore other brands
iFlow are exclusive distributors for MBS SRL
MBS SRL are experts in the heat treatment of Food, Drinks, Chemicals and Pharmaceuticals. Using quality raw materials and lean production methods, MBS manufacture a comprehensive range of Tubular Heat Exchangers and Scrape-surface Heat Exchangers for all types of fluid handling applications.
Explore other brands

iFlow are exclusive distributors for Debem
Debem hygienic Air Diaphragm Pumps are specially designed for handling an array of products in the Dairy, Food, Beverage, Cosmetics, Chemical and Pharmaceutical industries. Manufactured in high quality 316L, Debem Pumps offer complete flexibility and are ideal for ATEX pumping applications or handling products containing solids.
Explore other brands

iFlow are exclusive distributors for INCON tanks & vessels
Incon design and manufacture mobile stainless tanks ranging from 100 ltr to 2,500 ltr for use with storing and transporting a wide range of liquids. Many different designs are available to suit all types of applications including Tanks for use with Fork Trucks, Pallet trucks and Stand alone Tanks on wheels.
Explore other brands
iFlow are exclusive distributors for FBF Italia Homogenisers
FBF Italia design and manufacture Homogenisers and High-pressure Pumps to suit a wide range of applications in the food, Beverage, Chemical, Cosmetic and Pharmaceutical industries. Through many years of continuous research, FBF Italia continue to deliver high quality machines tailored to specific individual customer needs.
Copyright 2025 - Website design by Sian Evans Inc
Contact
+44 (0)208 180 2204
info@iflow.co.uk
Offices
UNIT A1B LORDS WOOD ROAD
HARWORTH, DONCASTER DN11 8BZ